Request a Quote: Call 781-890-3111

2026 Top Food Packaging Inspection Systems for Buyers

Food Packaging Inspection is not a single machine choice. It is a decision about which defects matter, where they can occur, and how quickly operators need to respond. A pinhole in a pouch, a missing seal, or a small metal fragment can each require a different inspection method. The right system depends on the product, package material, line speed, and acceptable false-reject rate.

Quality-management expert W. Edwards Deming is often associated with the reminder, “In God we trust; all others must bring data.” For buyers, that principle means asking vendors for test results using representative products and packaging—not relying on brochure claims alone. A trial should show how the system handles real variations, such as condensation on a tray or a crumpled label. Small details matter.

This guide to the 2026 Top Food Packaging Inspection Systems for Buyers compares technologies such as metal detection, X-ray inspection, vision systems, checkweighers, and seal inspection. It also considers integration, sanitation needs, changeover time, and the clarity of inspection records. No system is perfect. A camera may miss a defect hidden by glare, while an overly sensitive detector may reject good product. Buyers should examine those trade-offs before choosing. The sections ahead offer a practical framework for comparing options, validating performance, and asking sharper questions during supplier demonstrations. A checklist helps, but it cannot replace a well-designed production-line trial.
2026 Top Food Packaging Inspection Systems for Buyers

Food Packaging Inspection Systems: Scope, Line Placement, and 2026 Buyer Needs

Food packaging inspection systems cover several different checks, not one universal test. Depending on the product and package, a line may need to detect metal, verify package weight, inspect seals, or read printed codes. The right scope starts with the product, packaging material, and actual failure risks. A dry snack in a flexible pouch has different needs from soup in a metal can. Small details matter.

Placement affects results. An upstream check can catch a problem before filling, while a post-seal inspection can examine the finished pack. On a busy line, space, belt speed, vibration, and washdown routines all influence equipment selection. Ask suppliers to demonstrate performance using representative products and packaging, not just sample images or ideal conditions. Confirm how rejected packs are removed and how operators are alerted. Keep the process clear.

For 2026 purchasing, buyers should compare detection capability, inspection rate, changeover time, data records, and service support. Integration matters, too: a sensor that works well alone may create delays if it cannot communicate with the line. Plan for cleaning and routine verification before installation. No system removes every risk. Packaging variation can still confuse inspection, and overly sensitive settings may increase false rejects. That trade-off deserves a real production trial.

Food Safety Context: CDC Estimates 48 Million U.S. Foodborne Illnesses Annually

The CDC estimates that 48 million people in the United States experience foodborne illness each year. That figure gives packaging inspection a practical purpose beyond factory efficiency. A damaged seal, loose lid, or tiny metal fragment can create serious risk before a product reaches a family kitchen.

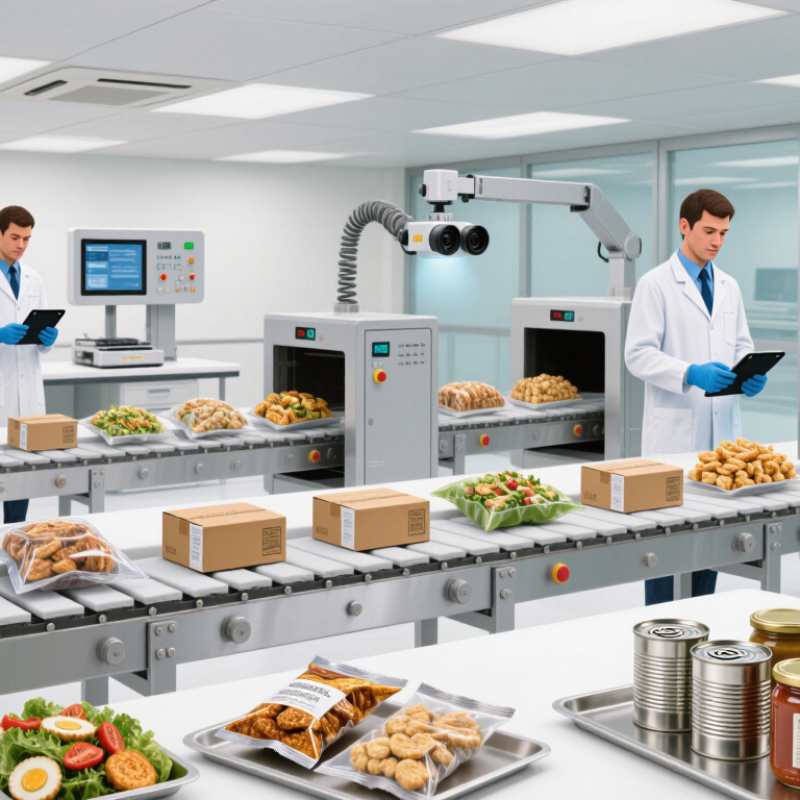
In 2026, buyers should examine inspection systems for seal integrity, foreign-object detection, label accuracy, fill levels, and package damage. Vision cameras can identify crooked labels and broken trays at production speed. X-ray inspection can reveal dense contaminants inside sealed products. Checkweighers can detect missing items or unusual weight changes. These tools work best when operators connect inspection results with batch records and sanitation checks.

Look closely at real operating conditions. A chilled line may produce condensation, glare, and cloudy film that confuse cameras. Ask for trials using your own packaging, products, speeds, and defect samples. The system should provide clear alarms, simple maintenance access, and controlled data storage. Staff also need practical training, not only software demonstrations.

No inspection system catches every defect. Sensor settings can drift. Operators can miss warnings during busy shifts. That weakness deserves honest review. Buyers should measure false rejects, missed defects, cleaning time, and response speed before approving a purchase. Independent validation and documented procedures can support safer decisions without replacing human judgment.

Metal Detection and X-Ray Inspection: Compare Contaminant Coverage and Test Methods

2026 Top Food Packaging Inspection Systems for Buyers

Metal Detection and X-Ray Inspection: Compare Contaminant Coverage and Test Methods

Choosing an inspection system starts with the contaminant risk, not the equipment label. Metal detectors identify ferrous, non-ferrous, and stainless-steel fragments. They work well on many dry products and sealed packs. However, salt, moisture, product temperature, and foil packaging can reduce sensitivity. A detector may perform differently after a recipe change.

X-ray inspection examines density differences inside the product. It can detect metal, glass, stone, mineral fragments, and some dense plastics. It may also reveal missing products or broken components. Yet low-density contaminants can remain difficult to find. Product shape matters too. A thick, uneven pack can hide a small fragment.

Test methods need realistic challenge pieces. Use certified test samples that match the product, package, and production speed. Place them at different positions, including the center and edges. Record every reject and confirm that the reject mechanism works. In plant trials, I have seen teams test only clean, stable packs. That creates confidence, but not always reliable evidence. Conditions change.

Test after startup, changeover, cleaning, and maintenance. Keep records of sensitivity, false rejects, and failed challenges. A practical comparison should include hygiene access, inspection speed, operator training, and data traceability. No system detects everything. The test plan must admit that limitation.

Checkweighing, Vision, and Seal Inspection: Verify Pack Quality and Label Accuracy

Checkweighing, vision inspection, and seal testing address different failure points on a food line. A checkweigher can flag packs above or below a configured weight range, while a vision system can compare printed dates, lot codes, and label placement against approved settings. Seal inspection adds another layer, detecting wrinkles, contamination, or inconsistent closure. Small defects matter. A sauce smear across the seal can be easy to miss during a fast visual check.

The USDA estimates that 30–40% of the U.S. food supply is lost or wasted, although that figure covers many causes and cannot be attributed to packaging defects alone (USDA, “Food Loss and Waste”). Still, sound packaging checks can help prevent avoidable product loss. Buyers should ask how systems handle changing pack sizes, reflective film, and blurred codes, then review test results from real production conditions. On paper, detection looks simple. On a busy line, it is less tidy. No single inspection method verifies weight, label accuracy, and seal integrity together, so acceptance criteria and routine challenge tests deserve careful attention.

2026 Top Food Packaging Inspection Systems for Buyers - Checkweighing, Vision, and Seal Inspection: Verify Pack Quality and Label Accuracy

Inspection System What It Checks Typical Detection Methods Common Applications Buyer Considerations
Dynamic Checkweigher Package weight while products move along a production line; can identify packs outside configured weight limits. Conveyor scale, load cell, product tracking, and configurable reject mechanism. Bags, cartons, trays, bottles, and other packaged foods. Confirm product size, line speed, weighing range, reject handling, calibration process, and integration with production records.
Vision Inspection Visible package and product features, such as presence, position, appearance, and selected print or label details. Industrial cameras, controlled lighting, image-processing software, and defined pass/fail rules. Checking label presence, cap or closure presence, product orientation, and visible packaging defects. Evaluate lighting, camera views, package variation, inspection criteria, changeover needs, and false-reject performance.
Label and Code Verification Whether selected label content, printed codes, or barcodes are present and readable against configured requirements. Optical character recognition or verification, barcode reading, and comparison with approved product data. Date and lot coding, barcode checks, label-to-product matching, and packaging line changeovers. Define which fields must be checked; validate code quality, print contrast, data setup, and recipe control.
Seal Inspection Visible seal characteristics, such as seal presence, position, continuity, or defects detectable by the selected method. Camera-based inspection or other application-specific non-destructive inspection methods. Flexible pouches, lidded trays, bags, and packages with defined sealing areas. A visual check does not necessarily prove hermetic integrity; establish defect limits and validate with appropriate seal testing.
Metal Detection Metal contamination that can be detected under the specific product, package, and equipment conditions. Electromagnetic detection with a configured reject or line-stop response. Packaged products on conveyor lines; application suitability depends on product and packaging characteristics. Assess product effect, package material, test procedures, reject confirmation, and the facility’s hazard-control plan.
X-ray Inspection Foreign objects or package features that create sufficient X-ray image contrast; configured systems may also check selected product attributes. X-ray imaging and image analysis, typically paired with a defined reject process. Packaged foods where inspection requirements and product characteristics justify X-ray screening. Detection depends on contaminant size, density, orientation, product, and packaging; review radiation-safety and maintenance requirements.

Performance and suitability depend on the product, package, line conditions, inspection setup, and validation results. Confirm acceptance criteria through trials using representative production samples.

Buyer Evaluation: Validate Detection Limits, Line Speed, Reject Controls, and 21 CFR 117

A food inspection system should be tested against the hazards identified in your product and process, not just a brochure’s best-case figure. Ask suppliers to demonstrate detection limits using representative packs, including different product temperatures, package materials, and positions on the belt. Record what the system detects and what it misses. Small details matter.

Then test at your actual line speed. A detector that performs well during a slow demonstration may behave differently when packages arrive close together or vary in size. Check reject timing with real production spacing, and confirm that rejected packs enter a locked or clearly monitored bin. Challenge tests should show that alarms, belt stops, and reject confirmations work as intended.

For facilities subject to 21 CFR Part 117, inspection equipment should fit into the food safety plan and its documented controls. Keep procedures for checks, calibration, corrective actions, and records clear enough for operators on every shift. The regulation does not make a particular machine suitable by itself; your hazard analysis and verification practices matter. Be honest about gaps. A test schedule can look complete on paper and still miss a rushed handoff between shifts.

2026 Top Food Packaging Inspection Systems for Buyers

Buyer evaluation: validate detection limits, line speed, reject controls, and 21 CFR 117 readiness.

Illustrative acceptance-test example only—not vendor or industry benchmark data. Confirm detection limits using representative products and challenge samples at the intended line speed; test reject timing, reject confirmation, and fault handling. 21 CFR Part 117 does not set universal inspection-system detection limits or line speeds. Assess applicable preventive-control, monitoring, corrective-action, and recordkeeping requirements with qualified food-safety personnel.